Ball Valves
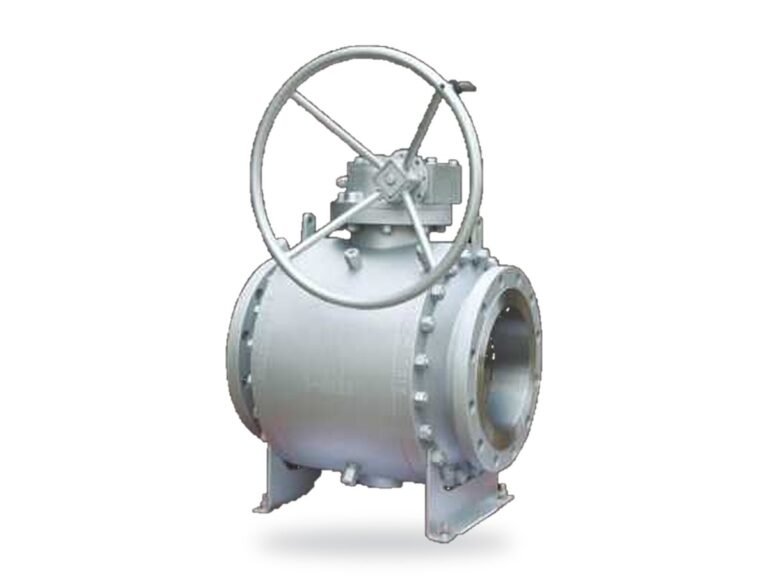
Forged steel trunnion ball valves have bodies and end closures machined from forged blocks rather than cast. Because forging does not produce casting defects such as gas porosity and shrinkage, they are preferred for high pressure classes, sour (H₂S) service and lines that require a compact installation.
Overview
Forged body valves are designed to API 6D and ASME B16.34 and can be selected from design families fire-tested to API 607. In high classes such as Class 900, 1500 and 2500, forging gives a more compact and lighter body for the same size.
Material can be LF2 for low-temperature service, or F316 or duplex F51 for corrosive service; NACE MR0175 / ISO 15156 requirements are documented through hardness records and the material certificate.
Technical specifications
| Pressure class | ASME Class 150–2500 (mainly 900–2500) |
|---|---|
| Size | 2″–60″ (DN50–DN1500); full or reduced bore |
| End connections | RF / RTJ flanged, butt-weld |
| Materials | A105N, A350 LF2, A182 F316, F51; other alloys on request |
| Design | Trunnion mounted, spring-loaded seats, antistatic, anti-blowout stem, fire-safe (API 607) |
| Testing | API 6D / API 598; gas testing and EN 10204 3.2 on request |
Key features
- Forged body: no casting defects such as gas porosity or shrinkage
- Compact, lighter construction at high pressure
- Design fire-tested to API 607
- NACE MR0175 compliant materials and hardness control for sour service
Catalog data
| Size and class | 2″–60″, Class 150–2500 (forged body; 2-piece in smaller sizes, 3-piece side entry in larger sizes) |
|---|---|
| Design and testing | API 6D, ASME B16.34; API 607 fire-tested design |
| Design features | Anti-blowout stem, anti-static design, ISO 5211 actuator mounting pad, double block and bleed (DBB), cavity pressure relief, low-emission packing, low torque |
Typical part materials
| Part | Carbon steel | Low temperature | Stainless (316) | Stainless (304) |
|---|---|---|---|---|
| Body, end caps | A105N | A350 LF2 | A182 F316 | A182 F304 |
| Ball, stem, seat ring | A105N + ENP | A350 LF2 + ENP | A182 F316 | A182 F304 |
| Seat insert | PTFE / RPTFE / PEEK | PTFE / RPTFE / PEEK | PTFE / RPTFE / PEEK | PTFE / RPTFE / PEEK |
| Spring | Alloy X-750 | Alloy X-750 | Alloy X-750 | Alloy X-750 |
| Stud bolts / nuts | A193 B7 / A194 2H | A320 L7 / A194 7 | A193 B8M / A194 8M | A193 B8 / A194 8 |
Documentation and testing
On industrial projects the documentation package matters as much as the valve. We confirm the certificate and test scope for every line item at quotation stage:
- EN 10204 3.1 material certificates for pressure-retaining and wetted parts, traceable by heat number
- EN 10204 3.2 with third-party inspection, on request
- Pressure test reports to API 598 or EN 12266-1: shell, seat and, where specified, gas tests
- Fire-test certificates (API 607 / ISO 10497) for fire-safe type-tested designs
- PMI reports for alloy and stainless materials
- Dimensional, visual and coating inspection records
- PED 2014/68/EU CE declaration for equipment within its scope
- NACE MR0175 / ISO 15156 compliance statement for sour (H₂S) service
Technical datasheet
Frequently Asked Questions
Why is a forged body more reliable than a cast body?
Forging consolidates the internal structure of the material, and defects that can occur in castings, such as gas porosity, shrinkage and sand inclusions, do not form. Forged bodies are therefore preferred for high-pressure and critical services.
Which tests are performed on forged valves?
API 6D / API 598 shell and seat tests are standard. For high-pressure gas service a high-pressure gas test is added, PMI for alloys, and, on request, EN 10204 3.2 certification witnessed by an independent inspector.
Related products
Floating Ball Valve
½”–10″, Class 150–600; two-piece and three-piece, fire-safe, antistatic.
View details
Trunnion Mounted Ball Valve
2″–60″, Class 150–2500; spring-loaded seats, DBB/DIB, sealant injection.
View details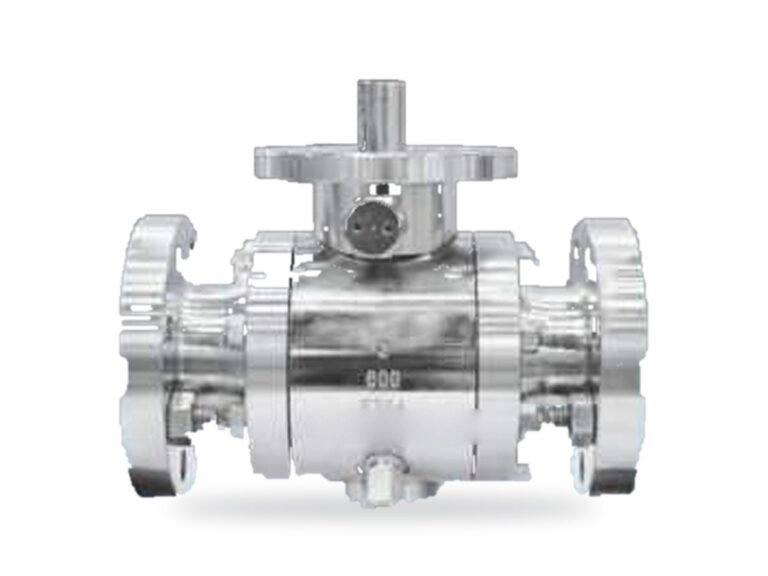
Metal Seated Ball Valve
Tungsten or chromium carbide coated ball and seats; abrasive and high-temperature service.
View detailsRequest a quote: Forged Steel Trunnion Ball Valve
Share your valve list, datasheet or project specification. We review standards, materials and documentation line by line and return an itemized offer, with any deviation from the specification stated in writing.